
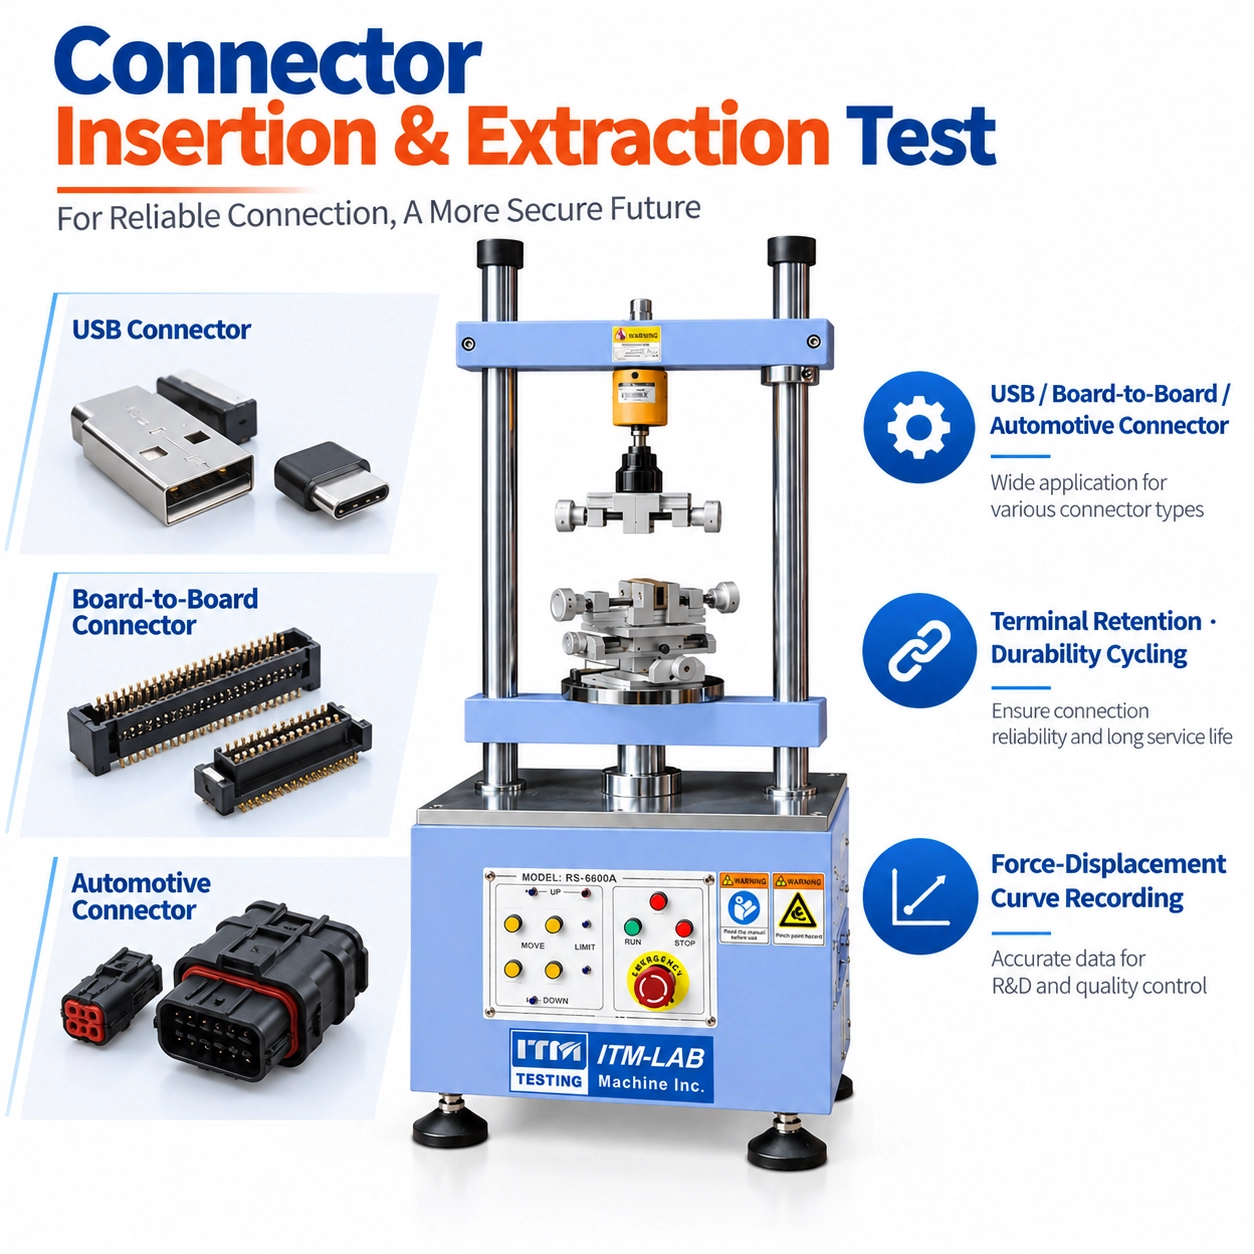
A connector that takes 42 N to mate and one that takes 68 N may both be electrically functional. Mechanically, however, they are not the same product.
Before deciding whether either result is acceptable, three questions need answers: What exactly was mated? At what speed? And against which product requirement?
That is the practical role of EIA-364-13.
EIA-364-13E, Mating and Unmating Force Test Procedure for Electrical Connectors and Sockets, provides a method for determining the forces required to mate and unmate electrical connectors, sockets and specified mating devices. Unless otherwise specified by the referencing document, Method A applies.
One distinction matters from the start:
EIA-364-13 defines the test method. It does not give every connector the same acceptable mating or unmating force.
The connector, product or customer specification may still define the test speed, specimen configuration, latch condition, force limits and other requirements.
That distinction is where a useful EIA-364-13 test begins.
【IMAGE 1 — INSERT HERE】
What EIA-364-13 Measures
Show an actual connector pair.
Left:
MATING
Plug → Receptacle
Right:
UNMATING
Plug ← Receptacle
Below, show a simple force-displacement trace.
Minimal labels:
Mating Force
Unmating Force
Bottom Caption:
Same interface. Two directions. Two mechanical force measurements.
Suggested Alt Text: EIA-364-13 connector mating and unmating force test
Image Size: 960 × 640 px
What EIA-364-13 Actually Measures
At its simplest, a mating test measures the force required to bring the specified connector interface into its mated condition. The unmating test measures the force required to separate it again.
That sounds straightforward until the connector reaches the fixture.
A real assembly may have two contacts or forty. It may include guide pins, polarization features, seals, a latch, PCB mounting or a cable bundle. Some specifications evaluate the actual connector pair; others require a defined gauge or mating device.
All of those details can change what the load cell sees.
For mating force, an unexpectedly high value may lead an engineer to investigate dimensional interference, contact loading, alignment, housing friction or another mechanical condition. An unexpectedly low unmating force may justify checking interface retention, contact wear, dimensional variation or changes after repeated mating cycles.
Neither value should be interpreted without considering the actual connector specification.
Method A vs Method B: Define What Is Being Mated
The EIA-364-13 scope accommodates connector mating configurations as well as connectors or sockets used with specified gauges or devices. Method A is used unless the referencing document specifies otherwise.
From a test-engineering standpoint, the useful question is simple:
What is the specified mating interface for this test?
With an actual mating assembly, the fixture needs to reproduce the intended relationship between the two components. Where a controlled gauge or mating device is specified, the fixture instead needs to hold that defined interface correctly and repeatably.
Do not select a configuration simply because it is easier to fixture. Check the controlled standard and the referencing product specification first.
| Test Consideration | Actual Mating Assembly | Specified Gauge / Device |
|---|---|---|
| What is evaluated? | Intended connector pair | Interface against defined mating geometry |
| Fixture holds | Both mating components | Connector/socket and specified device |
| Alignment concern | Mating axes of both components | Device-to-interface axis |
| Test condition source | Referencing specification | Referencing specification |
The difference becomes important when results from different laboratories are compared. A force value is only meaningfully comparable when the underlying mating configuration is comparable too.
【IMAGE 2 — INSERT HERE】
EIA-364-13 Test Configuration
Left:
ACTUAL MATING PAIR
Connector
↓
Mating Connector
Right:
SPECIFIED DEVICE
Connector / Socket
↓
Gauge / Device
Center:
EIA-364-13
Bottom Caption:
Confirm the required mating configuration before designing the fixture.
Suggested Alt Text: EIA-364-13 Method A Method B connector test setup
Image Size: 960 × 640 px
Define the Connector Before You Define the Machine Settings
One of the easiest ways to produce inconsistent connector-force data is to start programming the tester before the specimen condition has been defined.
For a repeatable test, record the connector pair or gauge, contact population, orientation and specimen history. Note whether the assembly is attached to a PCB, cable or housing and whether those parts influence how it can be fixtured.
Then look at the locking system.
Is the latch part of the measurement?
Not necessarily.
For example, a published TE Connectivity product specification referencing EIA-364-13 specifies mating and unmating measurements with the latches disengaged. It also defines product-specific force limits and a maximum test rate. Those conditions belong to that connector specification; they are not universal EIA-364-13 requirements.
Other connector families may handle locking features differently.
Before testing, answer a seemingly simple question:
Are you measuring the mating interface, or the complete mechanical action including the latch?
If that condition changes between tests, the results may no longer describe the same mechanical event.
【IMAGE 3 — INSERT HERE】
Does the Test Include the Latch?
Split visual.
LATCH DISENGAGED
Show connector mating interface only.
LATCH INCLUDED
Show latch mechanically engaging.
Bottom:
Follow the product specification.
Bottom Caption:
Connector configuration is part of the test condition.
Suggested Alt Text: connector mating force latch engaged disengaged
Image Size: 960 × 640 px
Fixture Design Matters More Than It Looks
A force tester only knows the load transmitted through its measurement axis. It cannot tell whether that load came from the contacts, the connector housing or a poor fixture.
Consider two connector halves that should mate on the same centerline.
If one is mounted at a slight angle, the machine can still push them together. The measured force, however, may now include lateral loading, guide-feature friction, housing interference and deformation caused by the setup itself.
A force peak caused by misalignment is still a real load-cell reading. It is simply not necessarily the connector behavior you intended to measure.
This becomes particularly important with high-density and multi-pin connectors, where several contacts and guiding surfaces may engage within a short travel distance.
Rigid or self-aligning?
A rigid fixture can work well when the connector geometry and mating axis are accurately controlled. It provides a stable, repeatable reference.
But greater rigidity is not automatically better.
If two rigid fixture halves are slightly out of alignment, the machine may force the connector to compensate for a setup error that would not exist in normal assembly.
A floating or self-aligning arrangement can be useful when required by the applicable specification or when limited freedom is needed to reproduce the connector's intended mating behavior.
There is no universal rule that every fixture should float or every fixture should be rigid. The correct approach depends on the connector and the specified test condition.
A useful check before collecting production data is to run several low-speed trial cycles and watch the specimen. If the connector visibly shifts, bends, twists or snaps into alignment during engagement, investigate the setup before treating the resulting force curve as baseline data.
【IMAGE 4 — INSERT HERE】
Connector Fixture & Alignment
Show three setups.
ALIGNED RIGID SETUP
Machine axis ↓
Connector axis ↓
MISALIGNED SETUP
Machine axis ↓
Connector axis ↘
Show:
Side Load
Extra Friction
SELF-ALIGNING SETUP
Show limited controlled alignment.
Bottom Caption:
The fixture should reproduce the intended mating condition—not add its own force.
Suggested Alt Text: connector mating force test fixture alignment
Image Size: 960 × 640 px
Test Speed: Follow the Referencing Specification
There is a recurring mistake in connector testing: someone finds a test speed in an old report or another connector datasheet and treats it as the EIA-364-13 speed for every product.
Published connector specifications show why that approach is unreliable.
One Molex specification referencing EIA-364-13 uses 25 ± 3 mm/min and defines mating force at 39.2 N maximum and unmating force at 2.45 N minimum. Another Molex specification uses 25 ± 6 mm/min and expresses its force requirements on a per-circuit basis.
The TE example mentioned earlier uses a maximum rate of 12.7 mm/min with the latches disengaged. A different TE connector specification uses 100 mm/min for its mating and unmating measurements.
Put those examples side by side and the point becomes clear:
| Published Example | Test Speed | Mating Requirement | Unmating Requirement |
|---|---|---|---|
| Connector A | 25 ± 3 mm/min | 39.2 N max | 2.45 N min |
| Connector B | 25 ± 6 mm/min | Product-specific / per circuit | Product-specific / per circuit |
| Connector C | ≤12.7 mm/min | 9.8 N/contact max | 0.9 N/contact min |
| Connector D | 100 mm/min | Product-specific | Product-specific |
These are examples of product-specific requirements, not values to copy into a new test plan.
The practical rule is:
Do not select test speed or force limits from the EIA-364-13 number alone. Check the specification that invokes the method.
【IMAGE 5 — INSERT HERE】
Same Standard. Different Test Conditions.
Center:
EIA-364-13
Three connector examples:
25 ± 3 mm/min
≤12.7 mm/min
100 mm/min
↓
PRODUCT SPECIFICATION
↓
TEST CONDITION + FORCE LIMIT
Bottom Caption:
Do not copy test conditions from another connector.
Suggested Alt Text: EIA-364-13 connector mating force test speed
Image Size: 960 × 640 px
A Practical EIA-364-13 Test Workflow
Once the requirement is clear, the laboratory sequence is relatively straightforward.
Start by identifying the controlled EIA-364-13 edition and the product or customer specification that invokes it. Record the required mating configuration, speed, specimen condition, latch state and acceptance criteria.
Next, prepare the connector in the required condition. A fully populated production connector and a partially populated engineering sample may produce very different forces. The same is true of a new specimen versus one that has already undergone repeated mating cycles.
Mount the specimen and establish the mating axis. Before collecting data, verify that the connector can complete the required travel without the fixture contacting the housing, cable, PCB or machine structure.
Run the mating stroke at the specified rate and record the force response through the required travel.
From the fully mated condition, perform the unmating stroke under the required conditions.
Finally, compare the measured values with the applicable product requirement.
For development work, retaining the complete force-displacement data is useful even when the formal acceptance criterion only requires a maximum or minimum force.
【IMAGE 6 — INSERT HERE】
EIA-364-13 Test Workflow
REQUIREMENT
↓
SPECIMEN
↓
FIXTURE + ALIGNMENT
↓
MATING
↓
UNMATING
↓
RESULT
↓
PRODUCT SPECIFICATION
Bottom Caption:
Control the setup first. Compare the force result second.
Suggested Alt Text: EIA-364-13 mating unmating force test procedure
Image Size: 960 × 640 px
Mating Force Is Not Terminal Retention Force
These terms are sometimes mixed together because they all involve pushing or pulling connector components. They do not answer the same engineering question.
Mating force describes the mechanical resistance as the specified connector interfaces come together.
Unmating force describes the resistance as those interfaces separate.
Terminal retention force concerns the ability of an individual terminal or contact to remain retained in its housing.
Crimp pull force asks a different question again: how strongly the conductor is mechanically retained by the crimped terminal.
A connector specification can contain several of these requirements side by side. Published connector documentation, for example, may reference EIA-364-13 for mate/unmate testing while assigning terminal retention to a separate test procedure.
| Test | What Moves? | What It Evaluates |
|---|---|---|
| Mating force | Connector pair moves together | Mechanical resistance during mating |
| Unmating force | Connector pair separates | Mechanical resistance during separation |
| Terminal retention | Terminal is pulled from housing | Contact-to-housing retention |
| Crimp pull | Wire is pulled from terminal | Wire-to-terminal crimp integrity |
Similar force-measurement hardware may be adaptable to more than one of these tests, but the fixture, specimen and interpretation are different.
That distinction is particularly useful when preparing an RFQ. "Connector pull force" alone is not enough information to define the test.
The Peak Number Is Only Part of the Story
Suppose two connectors both reach a peak mating force of 48 N.
If that is the only result stored, they look identical.
Now look at the complete force-displacement curves.
The first connector rises smoothly as the contacts engage and reaches its peak near the expected position.
The second shows a sharp 48 N spike halfway through travel, drops back, and then continues mating.
Those are very different mechanical behaviors.
A force-displacement trace helps show where resistance occurs, not just how large the maximum value became.
A relatively smooth curve may show gradual engagement followed by the principal mating peak and completion of the stroke. An early sharp spike may justify checking alignment, guide features, housing interference or an unexpectedly early contact event. A steep rise near the end of travel may justify checking for bottoming, latch engagement, dimensional interference or fixture contact.
These are diagnostic clues, not automatic diagnoses. The same curve shape can have more than one cause.
That is why the curve is most useful when combined with specimen inspection and knowledge of the connector geometry.
【IMAGE 7 — INSERT HERE】
Reading a Connector Force-Displacement Curve
Three curves:
A — SMOOTH ENGAGEMENT
Gradual force rise.
B — EARLY SPIKE
Highlight early peak.
Check alignment / interference
C — LATE SHARP RISE
Highlight end-of-travel rise.
Check bottoming / latch / geometry
Small note:
Diagnostic examples—not universal pass/fail curves.
Bottom Caption:
Peak force tells you how much. Displacement helps show where.
Suggested Alt Text: connector mating force displacement curve analysis
Image Size: 960 × 640 px
Worked Example: Configuring a Connector Mating Test
Consider a hypothetical 24-position connector.
The following values are used only to demonstrate equipment-selection logic. They are not EIA-364-13 limits.
| Requirement | Example |
|---|---|
| Expected peak mating force | Approx. 70 N |
| Test speed | 25 mm/min |
| Required movement | 32 mm |
| Test direction | Mating + unmating |
| Latch | Disengaged |
| Required output | Peak force + force-displacement curve |
Start with force capacity.
A 70 N expected peak is approximately 7.1 kgf.
A 5 kgf configuration cannot cover that expected peak and can therefore be eliminated.
A 10 kgf range nominally covers 70 N, but it leaves limited headroom. If sample variation or an abnormal specimen can exceed the expected value, that needs to be considered.
A 20 kgf configuration provides substantially more capacity. Whether it is the better choice depends on the actual sensor specification, required measurement resolution, overload allowance and expected variation.
The point is not that 20 kgf is always the correct choice for a 70 N connector.
It is that the force range should be selected from the actual test envelope instead of defaulting to the highest available machine capacity.
Next comes travel. A required 32 mm movement is comfortably within a system providing 150 mm of test stroke.
The requested 25 mm/min rate is also within a tester designed for controlled low-speed movement.
At this stage, the fixture may be the most application-specific part of the configuration. A 24-position connector can generate substantial side loading if its mating halves are held off-axis. Connector drawings—or preferably a physical sample for unusual geometries—help define the fixture before manufacture.
The resulting equipment specification can now be written much more clearly:
Appropriate force range + 25 mm/min controlled motion + at least 32 mm usable movement + connector-specific fixture + force/displacement recording
That is a better purchasing specification than simply requesting a "100 kgf connector tester."
【IMAGE 8 — INSERT HERE】
Connector Test Setup Example
Show an actual connector test arrangement.
24-POSITION CONNECTOR
Callouts:
≈70 N
25 mm/min
32 mm travel
Latch disengaged
↓
FORCE RANGE
FIXTURE
STROKE
FORCE + DISPLACEMENT
↓
Use actual ITM-LAB RS-6600A.
Bottom Caption:
Configure the test system around the expected mechanical test envelope.
Suggested Alt Text: connector force tester load cell selection example
Image Size: 960 × 640 px
Where Connector Force Data Goes Wrong
When repeated results are inconsistent, the load cell is not always the first thing to blame.
The connector is off-axis. Even a small angular error can add friction or housing interference.
The fixture position changes between specimens. A connector that seats against a different reference surface each time is not being tested under the same mechanical condition.
The latch state is inconsistent. One specimen is tested with the latch disengaged; another includes latch engagement.
The test speed came from the wrong specification. A rate used for a previous connector family was copied into the new program without checking the applicable requirement.
The connector history is unknown. A new specimen is compared with one that has already been mated repeatedly.
The selected force range is unnecessarily large. Maximum machine capacity and the most appropriate measurement range are not the same question.
The cable or PCB is loading the specimen. A stiff cable bundle can introduce preload or a bending moment before mating even begins.
These are ordinary setup problems, but they can make otherwise good force data difficult to compare.
A useful laboratory habit is to save the setup information together with the numerical result. A force value without its configuration is much less useful six months later.
Selecting Equipment for EIA-364-13 Testing
The right connector force tester is not simply the one with the highest load capacity.
Start with the expected mating and unmating loads and select a force range that covers them with appropriate headroom. Consider the measurement resolution needed for the application rather than selecting maximum capacity by default.
Next, confirm speed and stroke.
The machine needs enough usable movement for the complete test, not just the nominal engagement length of the connector. Fixture geometry and approach position can consume additional travel.
Working space matters too. A small connector mounted on a PCB or attached to a cable assembly may require considerably more fixture clearance than its housing dimensions suggest.
Finally, decide what data the test needs to produce.
For a straightforward acceptance check, the applicable peak mating or unmating value may be sufficient. For engineering comparison, supplier evaluation or failure analysis, synchronized force and displacement data provide considerably more context.
RS-6600A for Connector Mating & Unmating Force Testing
The ITM-LAB RS-6600A Connector Insertion & Extraction Force Tester is designed for controlled mating, unmating and related connector force measurements.
Available force capacities of 5, 10, 20, 50 and 100 kgf allow the measurement range to be selected around the application rather than using one capacity for every connector.
The system provides a 0–150 mm test stroke and configurations with test speeds of 0.01–300 mm/min or 0.01–600 mm/min. A Panasonic servo motor controls the test motion while the system records force together with displacement.
| Parameter | RS-6600A |
|---|---|
| Force capacity | 5 / 10 / 20 / 50 / 100 kgf |
| Test stroke | 0–150 mm |
| Test speed | 0.01–300 or 0.01–600 mm/min |
| Displacement resolution | 0.001 mm |
| Force units | N, kN, gf, kgf, lb |
| Equipment accuracy | Level 0.5 |
| Drive system | Panasonic servo motor |
| Fixture | Configurable to connector geometry |
The final fixture should be selected or designed around the actual connector geometry, mating direction and required test condition.
For a new application, connector drawings and photos are usually more useful than the connector name alone.
【IMAGE 9 — INSERT HERE】
EIA-364-13 Test System Selection Roadmap
WHAT CONNECTOR ARE YOU TESTING?
↓
PRODUCT / CUSTOMER SPECIFICATION
↓
REQUIRED TEST CONFIGURATION
↓
MATING / UNMATING / BOTH?
↓
LATCH CONDITION
↓
EXPECTED FORCE
↓
Three branches:
FORCE
LOAD RANGE
MOTION
SPEED + STROKE
FIXTURE
CONNECTOR GEOMETRY
Merge:
↓
ALIGN MATING AXIS
↓
PEAK ONLY OR FORCE + DISPLACEMENT?
↓
PASS / FAIL REQUIREMENT
↓
CONFIGURE RS-6600A
Use the actual ITM-LAB RS-6600A at the bottom.
Bottom Caption:
Define the connector requirement first. Configure the tester second.
Suggested Alt Text: EIA-364-13 connector force test system selection roadmap
Image Size: 960 × 1440 px
What to Send When Requesting a Connector Force Test System
For a standard connector pair, fixture selection may be straightforward. For an unusual housing, PCB-mounted assembly or multi-pin connector, a little application information saves a lot of back-and-forth.
Useful information includes:
Connector manufacturer / part number · Plug and receptacle drawings · Overall dimensions · Contact count · Expected mating and unmating force · Required speed · Required travel · Latch condition · Applicable EIA-364-13 / product specification · Required output · Connector photos or samples
For a custom fixture, a dimensional drawing is particularly useful. A physical sample may be preferable for complex geometries.
The objective is to define the actual load path before the fixture is manufactured.
Frequently Asked Questions
Does EIA-364-13 specify the mating force limit?
Not as one universal value for all connectors. EIA-364-13 provides the mating and unmating force test method; the applicable connector, product or customer specification determines the relevant acceptance limits. Published connector specifications referencing EIA-364-13 use different limits for different interfaces.
What speed should I use for an EIA-364-13 test?
Use the rate required by the applicable test and referencing product specification rather than copying a speed from another connector. Published product specifications referencing EIA-364-13 demonstrate that different connector families can use substantially different test rates.
Should the connector latch be engaged during the test?
Only if that is the required test configuration. Some published specifications explicitly require mating and unmating measurements with the latch disengaged. Always check the applicable connector or customer specification.
Is mating force the same as terminal retention force?
No. Mating and unmating force describe the interaction between mating connector interfaces. Terminal retention evaluates how well an individual contact remains retained in its connector housing. These are separate mechanical tests and may use different procedures and fixtures.
What load-cell range should I use for connector force testing?
Start with the expected maximum test force, then consider sample variation, required headroom, measurement resolution and the actual sensor specification. Selecting the highest available capacity by default is not necessarily the best measurement strategy.
One Standard Number Is Not a Complete Test Plan
EIA-364-13 provides connector engineers with a common method for mating and unmating force measurement. It does not remove the need to understand the connector being tested.
Before the first specimen goes into the fixture, you should know what is being mated, whether the latch is included, which speed applies, what force requirement applies, how the mating axes will be aligned and whether you need a peak value alone or the complete force-displacement response.
Once those questions are settled, selecting the equipment becomes much easier.
For the ITM-LAB RS-6600A, the test system can then be configured around the required force range, test speed, stroke, fixture and data output, rather than around machine capacity alone.
Define the connector requirement first. Configure the force tester second.
